Packaging Masterbatch Solutions
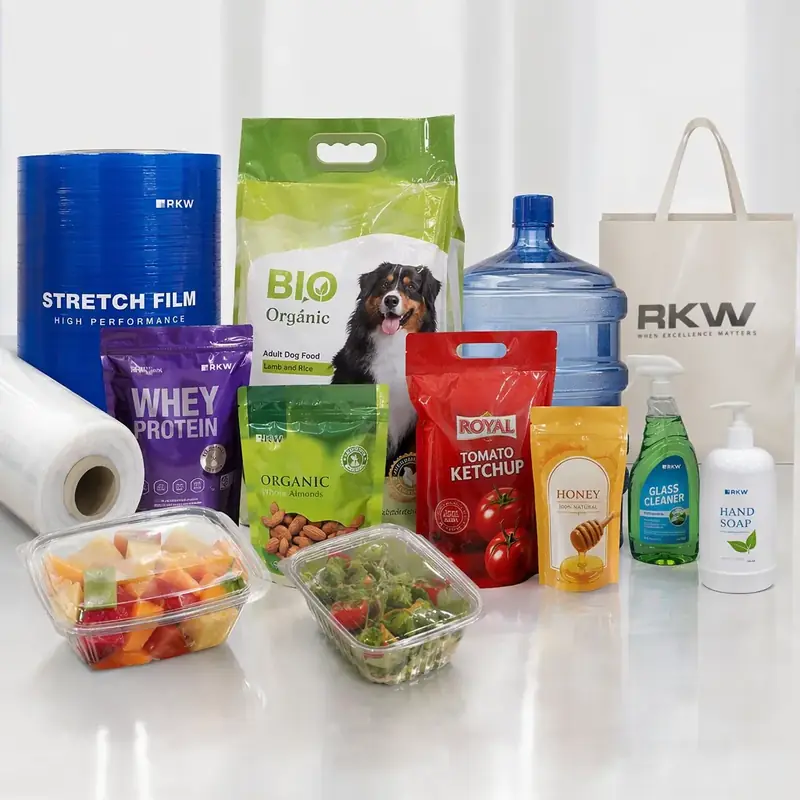
Food-grade color and additive masterbatch solutions for flexible films, rigid containers, PET bottles, and closures — engineered for safety, color consistency, and high-speed production efficiency.
Industry Challenges
Packaging manufacturers face a unique set of demands when coloring plastics destined for direct or indirect food and beverage contact. The stakes are high: a single color inconsistency or compliance gap can halt production lines, trigger costly recalls, and damage a brand's reputation. At the same time, packaging must be lightweight, cost-effective, and increasingly recyclable — all while looking flawless on the shelf.
- Strict food safety compliance with FDA, EU 10/2011, and GB 9685 regulations for every pigment and additive
- Consistent color across high-speed, multi-line production where even minor drift becomes visible to consumers
- High dispersion quality for thin films and lightweight containers that leave no room for specks or streaks
- Low-temperature processing compatibility for heat-sensitive resins such as LLDPE and PET
- Cost efficiency without compromising visual appeal in a price-sensitive market
- Recyclability and NIR-detectable options to meet growing sustainability requirements
- Chemical resistance for aggressive contents such as detergents, oils, and acids
- UV and light stability to protect packaged goods from fading on store shelves
Our Solution
MHK Color provides food-grade masterbatches engineered specifically for packaging performance, backed by a 30,000+ formulation database and a dedicated color-matching team.
- FDA and EU 10/2011 compliant formulations for direct food and beverage contact
- High-dispersion grades that deliver flawless thin films with no specks or streaks
- Low-temperature processing options for heat-sensitive resins
- NIR-detectable black masterbatch for fully recyclable packaging
- Rapid color matching with 24-hour sampling to accelerate product launches
- Batch-to-batch consistency of Delta E < 1.0 for worry-free production
- High-opacity white masterbatch for rigid containers and closures
- Anti-block and slip additives for smooth film handling and conversion
From flexible films to rigid containers and PET bottles, our packaging masterbatches combine safety, visual appeal, and processing efficiency to keep your lines running and your brand looking its best.
Explore Packaging Applications
Flexible Film Packaging
Color and additive masterbatch for blown film, cast film, and multi-layer flexible packaging with flawless dispersion and food-contact safety.
Rigid Containers & Closures
High-opacity color masterbatch for injection and blow molded containers, caps, and closures with premium appearance.
PET Bottles
Food-contact color masterbatch for PET bottles and preforms, engineered for clarity, color stability, and recyclability.
Recommended Products
Color Masterbatch
Standard stock color masterbatch in 12 color families for polyolefin applications, backed by 25 years of formulation expertise and a 30,000+ color database for all polymer types, with a complete QC process ensuring color consistency.
Functional Additives
UV stabilizer, antistatic, antioxidant, slip, antiblock, desiccant and laser-marking masterbatch.
Black Masterbatch
High-concentration carbon black masterbatch delivering superior opacity and stable dispersion. Batch consistency is our core focus, with UV-resistant and NIR-detectable grades available.
White Masterbatch
White masterbatch with 20% to 75% rutile titanium dioxide, engineered for optimal opacity and outdoor weather resistance.
Need a solution for your packaging application?
Our technical team is ready to help you find the right masterbatch formulation.